



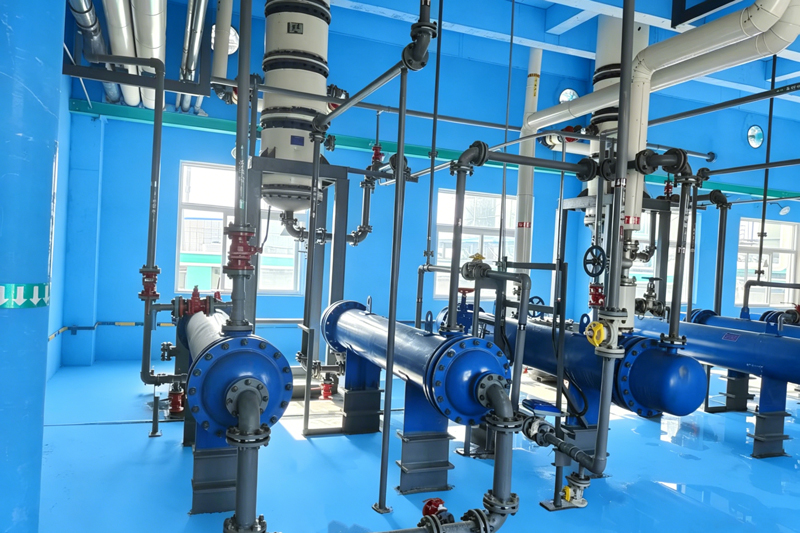
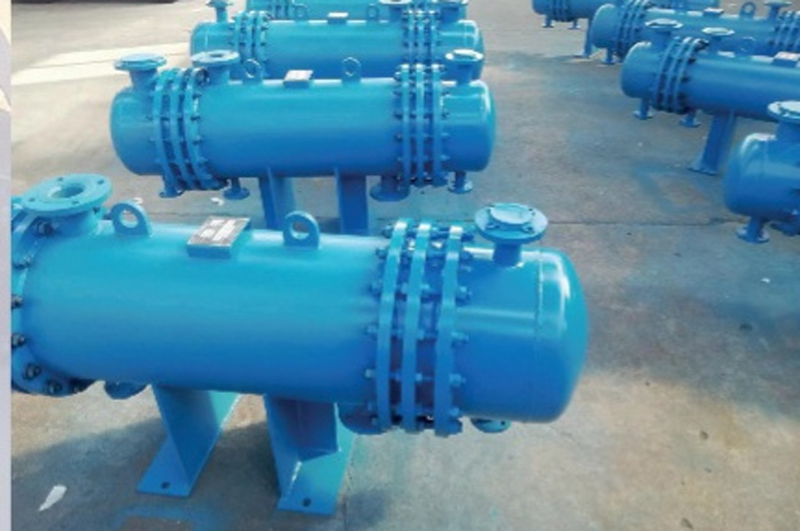
High-Efficiency Condensation & Separation Unit, Overview of Condensation and Separation Systems for Bromine Extraction
Technical Characteristics
Condensation and Separation Process Introduction:
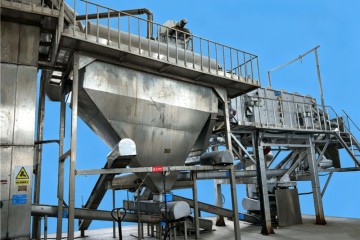
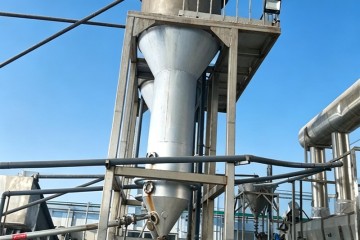
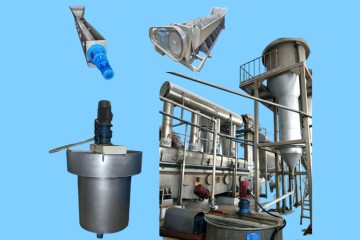
As the key backend equipment for air blowing-out method, distillation method, and steam stripping method bromine extraction processes, this unit undertakes the critical task of condensing high-temperature bromine-containing vapor and separating gas-liquid phases.
Working Principle of the Condenser
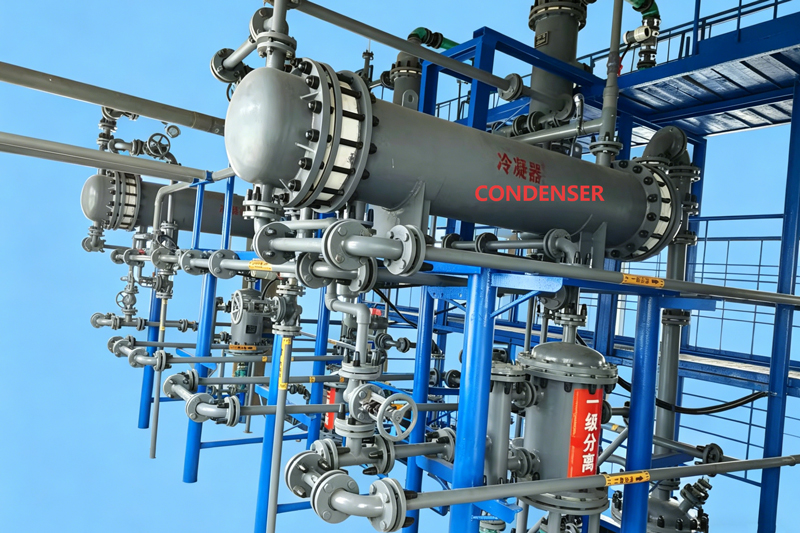
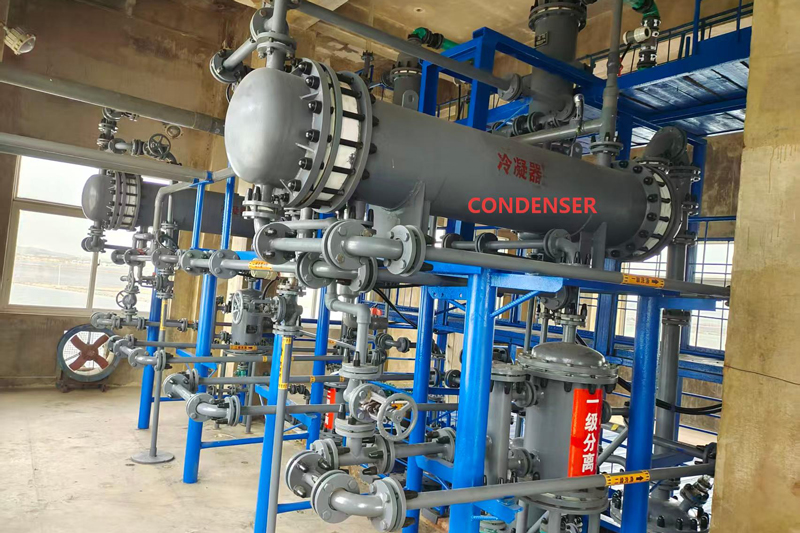
The core function of the condenser is to cool and liquefy the bromine-containing vapor produced in the distillation process, laying the foundation for the subsequent purification of bromine. It is a key device connecting distillation and refining .
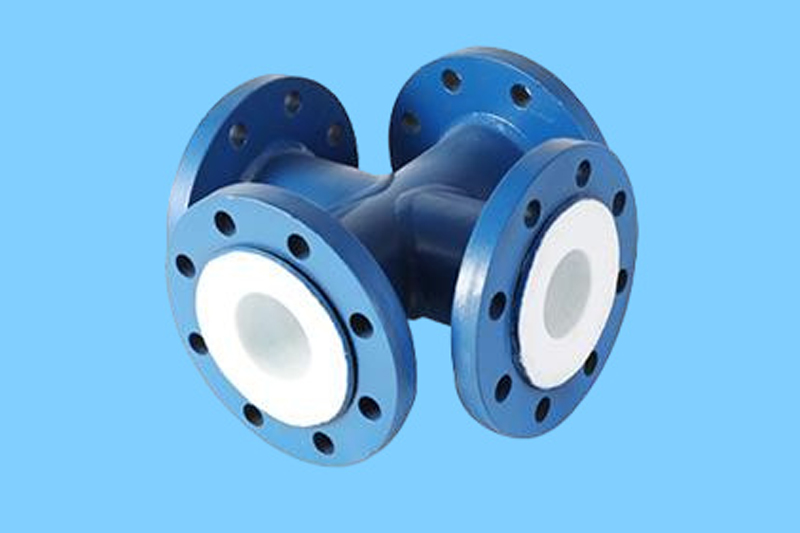
Feed: After the distillation tower is heated, the bromine-containing absorption liquid (sodium bromide, hydrogen bromide, etc.) will evaporate to produce bromine-containing vapor (mainly bromine vapor, with a small amount of water vapor and acidic gases), which is transported through pipelines to the condenser.All equipments are specially treated by PTFE to assure corrosion resistance.
Cooling and Liquefaction: The condenser is equipped with heat exchange tubes. Inside the tubes, a cooling medium (usually cooling water) is passed, while outside the tubes is the bromine-containing vapor. By heat exchange, the heat of the bromine-containing vapor is absorbed by the cooling medium, and the temperature rapidly drops below the cooling point of bromine , causing the vapor to condense into liquid crude bromine (containing a small amount of water and impurities).
Discharge: The condensed liquid crude bromine is transported through the bottom pipeline of the condenser to the separator for the next purification step. The cooling medium, after absorbing heat, warms up and is discharged through the circulation pipeline. After cooling, it can be reused.
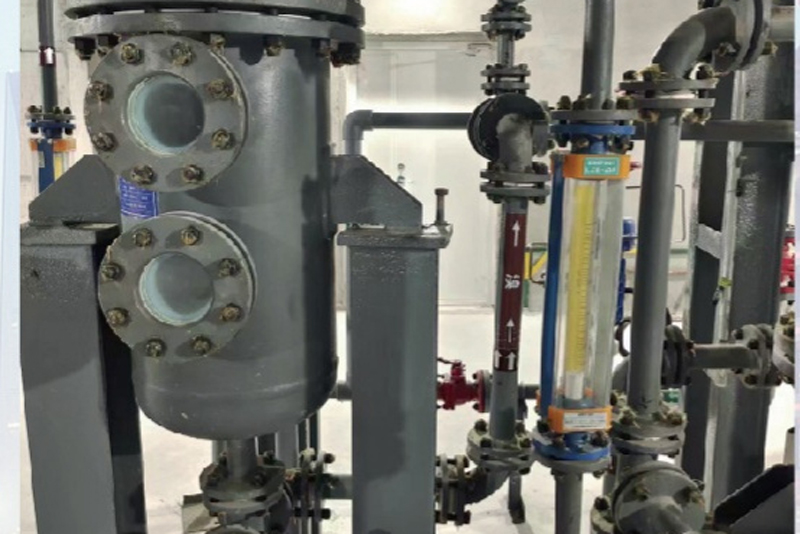
Liquid crude bromine enters the separator, where it is separated into layers by the density difference between bromine and impurities (the density of bromine is approximately 3.12 g/cm³, which is much greater than that of water at 1 g/cm³). The bromine at the bottom of the separator is discharged through the outlet and enters the subsequent refining process.
Below is silicon carbide heat exchanger .
Technical Specifications
| Design Temperature | -20℃ ~ 180℃ (adapt to high-temperature bromine vapor cooling) |
| Heat Exchange Area | 10 m² ~ 500 m² (customized according to production capacity: 1,000 t/a ~ 50,000 t/a bromine production line) |
| Cooling Medium | Circulating cooling water |
| Service Life | ≥ 10 years (core heat exchange components); (suitable for 24/7 continuous industrial production) |
Multi-Pass Flow Division Condensation Design: Utilizes multi-channel flow division to reduce vapor velocity and prolong heat exchange duration. The overall heat transfer coefficient is increased by 30% compared to conventional single-pass equipment, achieving bromine vapor condensation more efficiency and effectively minimizing volatilization loss.
• Multi-Stage Gas-Liquid Separation Structure: Combines primary and secondary separation vessels for precise separation of liquid bromine, brine, and non-condensable gases. Bromine purity rate is enhanced by 1%–8%, providing high-purity feedstock for subsequent refining processes.
• Optimized Flow Path Design: Prevents liquid accumulation and gas blockage to ensure continuous and stable material flow, accommodating high-volume industrial production requirements.