


Leave Your Message
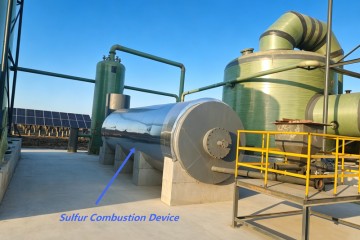
High-efficiency sulfur burning system designed for generating pure SO2 gas, optimized for industrial bromine extraction and acidic chemical synthesis.
 Brand: Ruitu Automation
 Origin: China
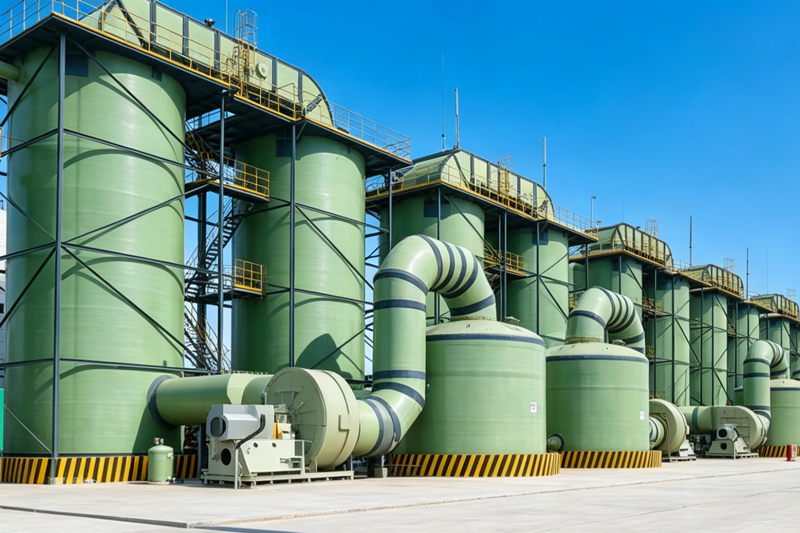
Complete turnkey solutions for industrial-scale bromine extraction from underground brines and chemical tail waters, adapted for low-temperature operation.
Brand: Ruitu Automation
Origin: China
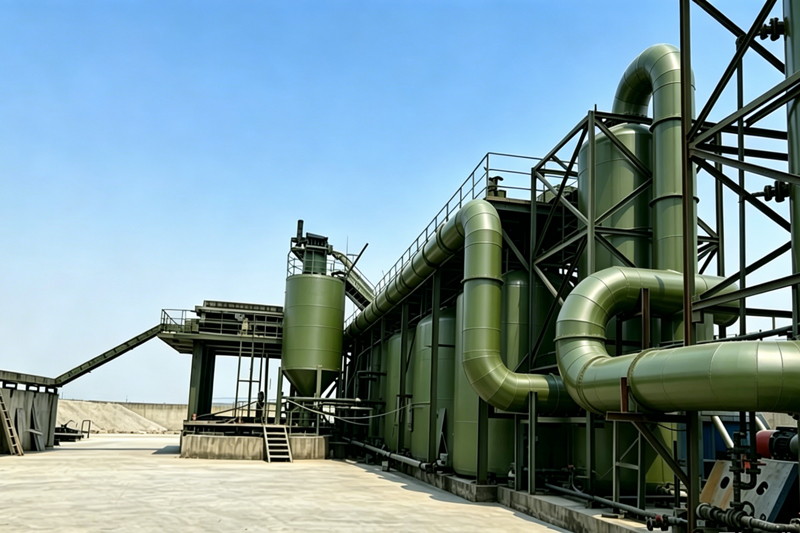
Highly adaptable equipment for processing raw calcium salts, featuring high efficiency and precise thermal control for cold-climate applications.
Brand: Ruitu Automation
Origin: China
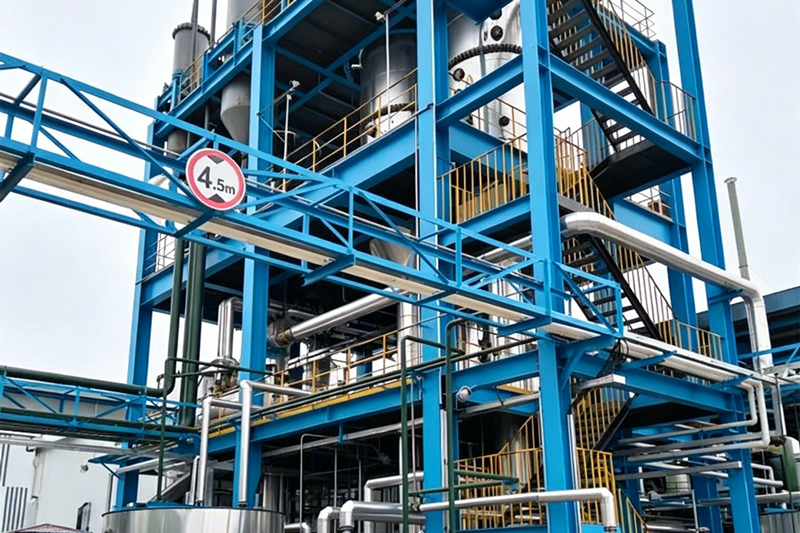
Specially designed system to extract magnesium chloride from seawater, salt lake brine, and chemical processing byproducts.
Brand: Ruitu Automation
Origin: China
The industrial sector in Russia, particularly in regions such as the Urals, Siberia, and the Volga Federal District, relies heavily on advanced chemical processing technologies. The demand for reliable China Sulfur Combustion Devices has grown exponentially as Russian chemical complexes modernize their systems to process complex minerals, manufacture agricultural fertilizers, and refine local petroleum products. Sulfur furnaces play a critical role in these setups by providing a stable, high-yield source of sulfur dioxide (SO2), which is essential for sulfuric acid production, bleaching processes, and the extraction of active chemicals like bromine from subterranean brines.
Operating chemical machinery in the sub-zero conditions of Russian winters requires specialized design modifications. Chinese manufacturing facilities serving Russia, such as Ruitu Automation, specialize in constructing sulfur combustion devices with advanced thermal insulation and automated heating systems. These systems prevent liquid sulfur solidification in the feed lines and maintain optimal reaction chamber temperatures even when ambient conditions drop below -40°C.
Modern Russian environmental standards (Rosprirodnadzor) demand strict control over industrial emissions. Consequently, the trend in sulfur combustion technology is moving toward high-efficiency burners that ensure complete oxidation of sulfur with zero unburnt residues. Incorporating smart automation, oxygen enrichment systems, and dual-stage heat recovery boilers allows factories to lower fuel consumption while generating high-pressure steam for auxiliary plant power. Ruitu Automation integrates real-time sensors and digital control panels, enabling operators to remotely monitor combustion parameters, ensuring stable gas generation and safe operations.
Founded in 2015, the company is located in Binhai Economic and Technological Development Zone, Weifang City, Shandong Province, covering an area of 28,000 square meters. With over a decade of experience in salt chemical equipment manufacturing, we are an EPC contractor specializing in salt chemical equipment, providing comprehensive services from water quality testing, plant site selection, equipment production, process formulation, installation and commissioning, production guidance to product recycling and dismantling of decommissioned projects. We provide satisfactory salt chemical equipment solutions for customers in multiple countries.
Years Experience
Sqm Factory Area
Full Turnkey Service

OUR BUSINESS • EPC SERVICE
Siberian Bromine Extraction Project Case
Urals Salt Washing Project Case
Volga Region Salt Chemical Project Case
When clients need new projects, our company organizes relevant technicians who have rich experiences to analyze the local resources, then provides a brief quotation and economic benefit analysis covering the overall construction of the project plant based on the client's budget and expected daily processing capacity.
VIEW DETAILS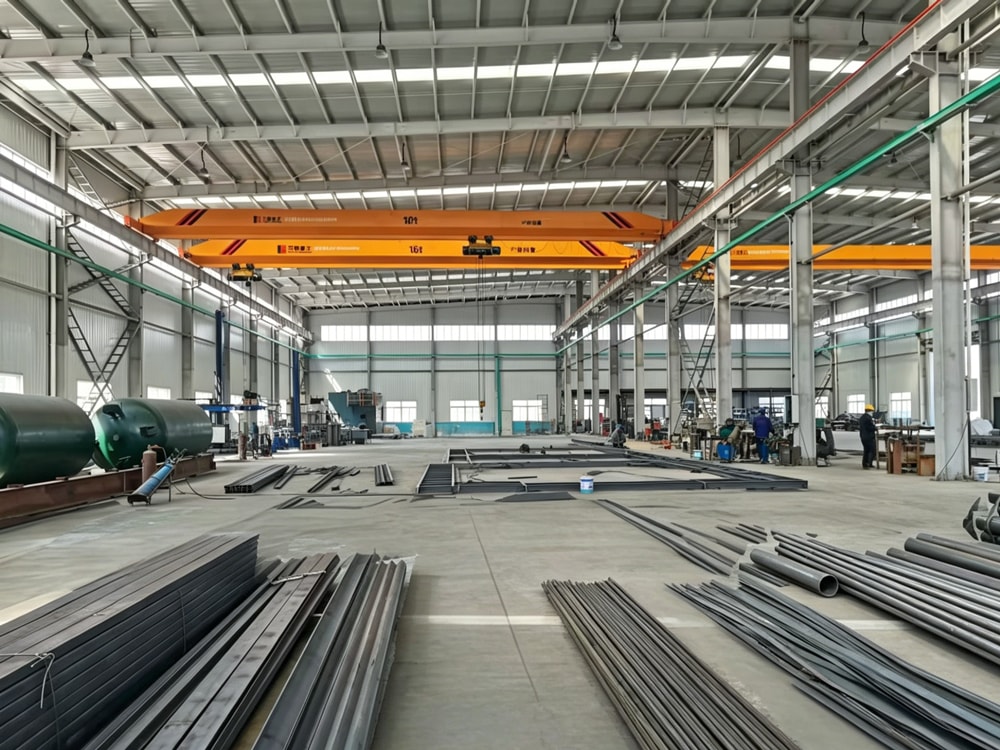
With a mature and compete procurement and supplier management system, RUITU Automation Equipment Company has established long-term cooperation relations with Influential and excellent suppliers in the industry.
VIEW DETAILS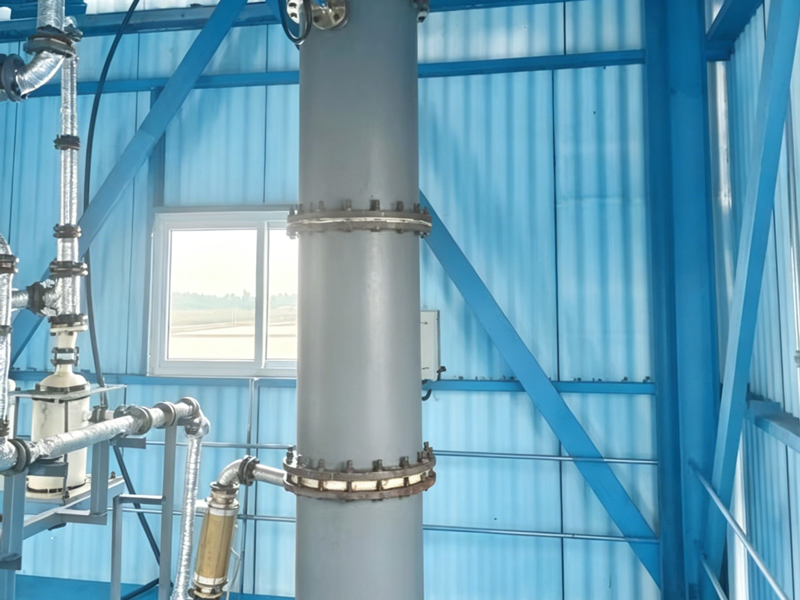
The equipment installation and commissioning have been completed, and the production of finished products has begun. Finished products reach the production capacity designed for the customers’ requirement, achieve the expected daily processing capacity.
VIEW DETAILS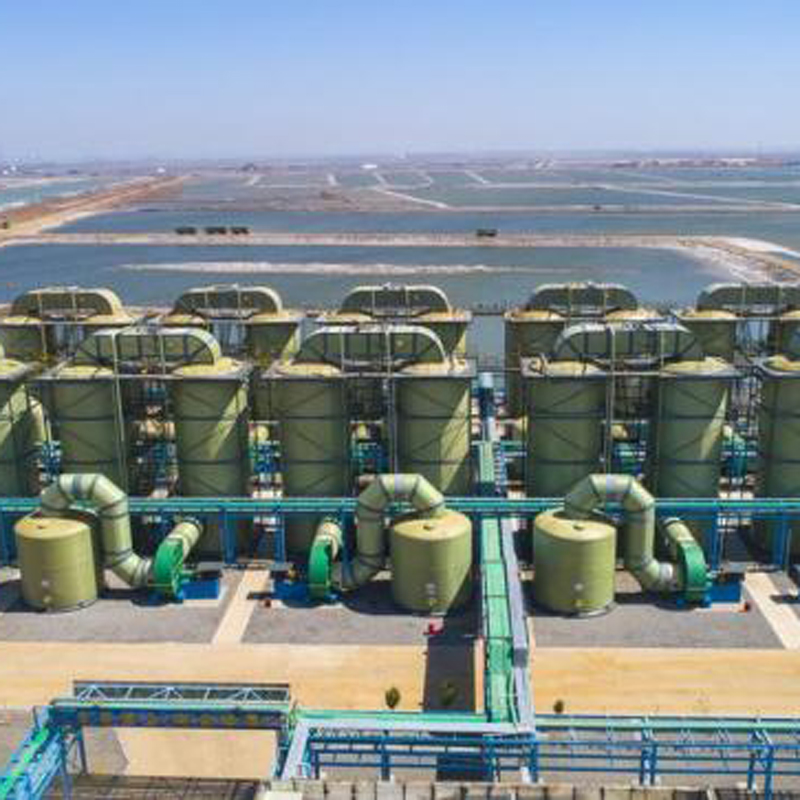
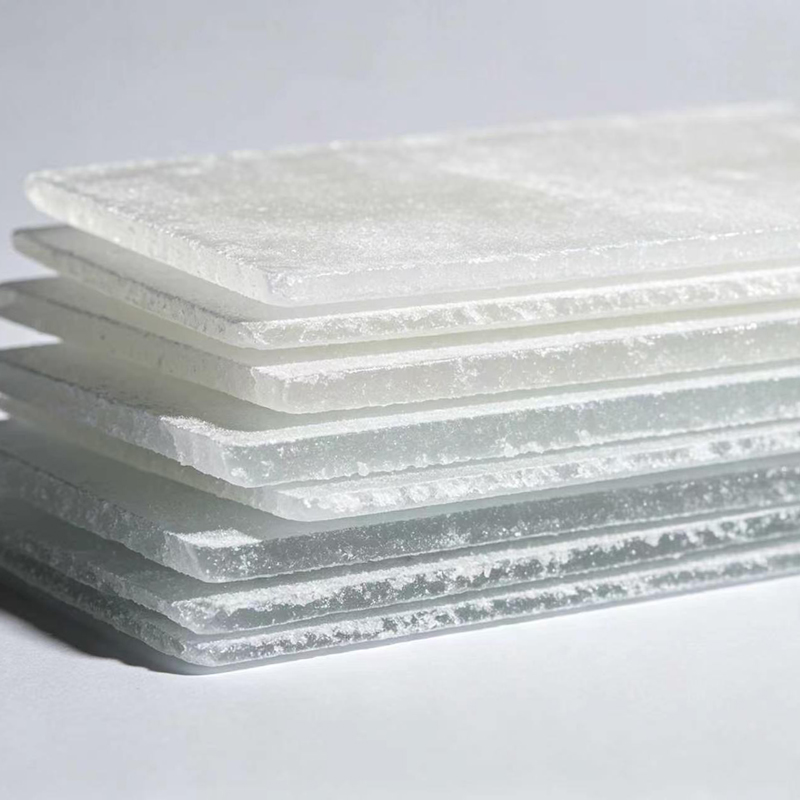
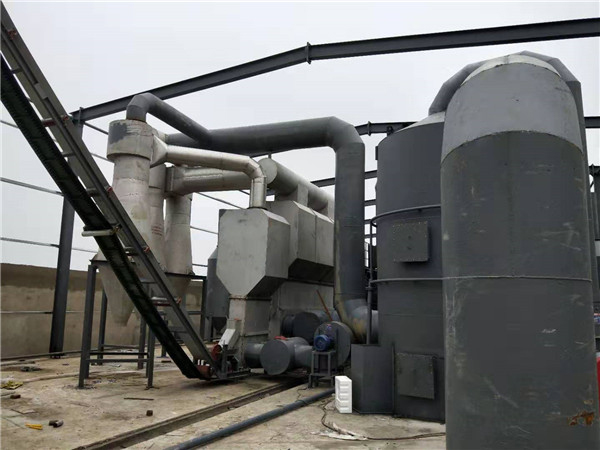
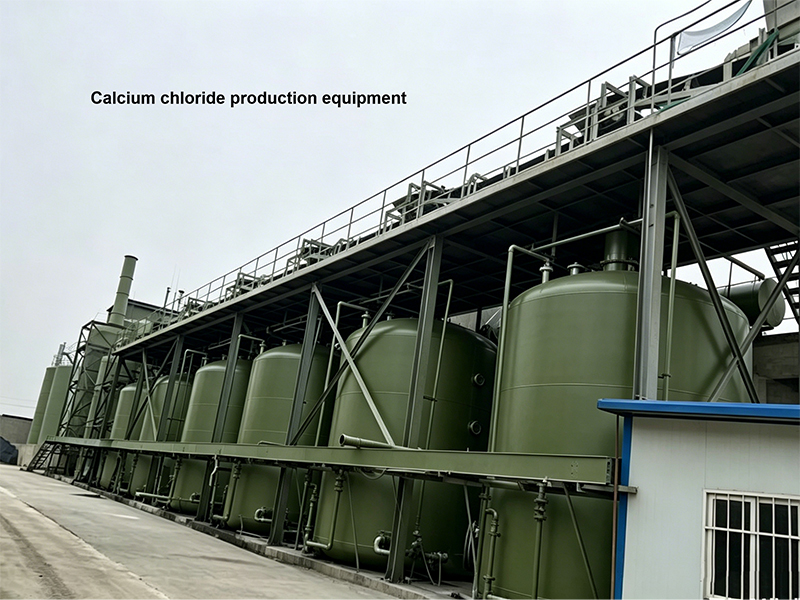
The chlorine gas calcium chloride process equipment consists of key components including a reactor, absorption tower, and purification system, designed for high output and low energy consumption.
May 11, 2026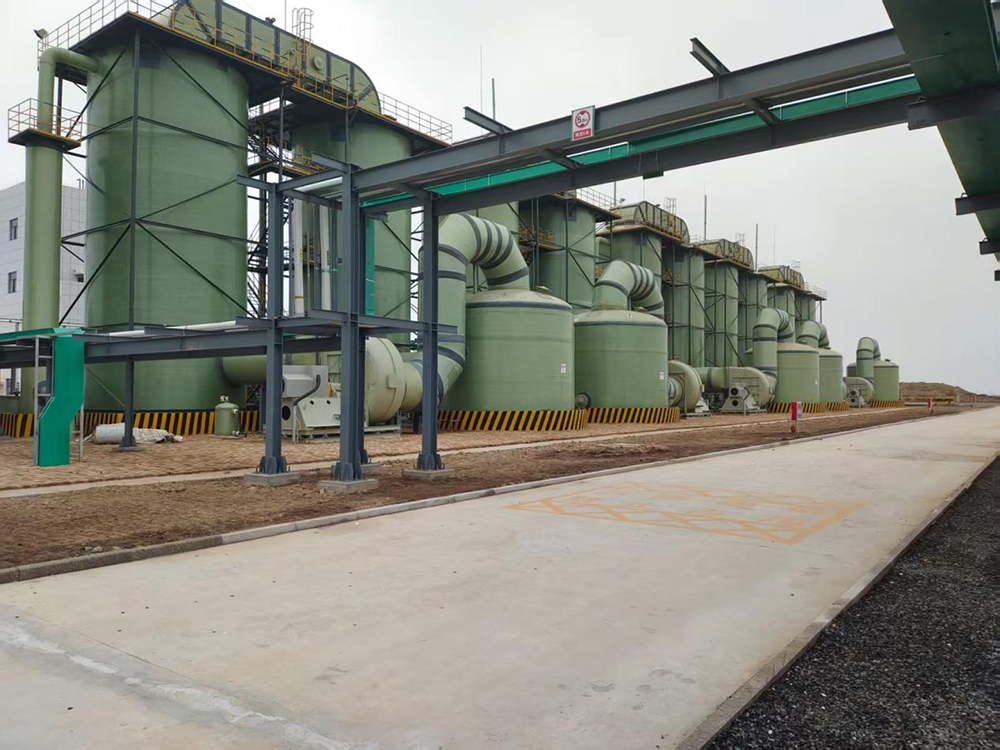
Bromine is known as the "marine element," with over 99% of Earth's bromine reserves stored in the ocean. Learn how customized sulfur combustion units assist in highly efficient extraction lines.
May 11, 2026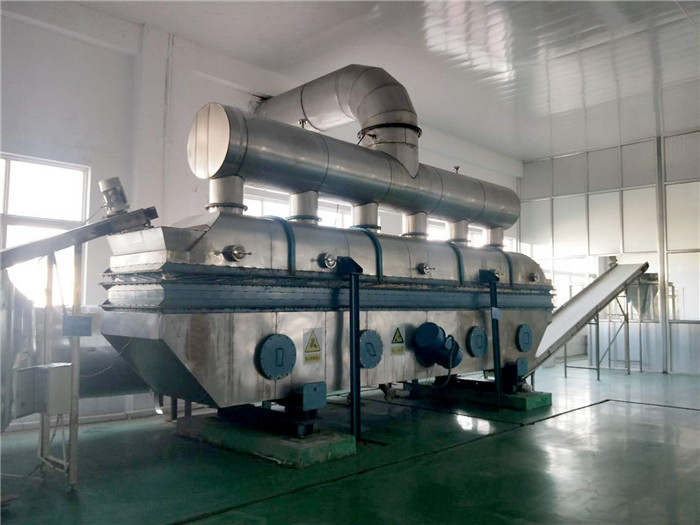
With the development of fluidized bed drying application technology, various types of fluidized bed dryers have been successfully integrated into salt purification lines.
May 11, 2026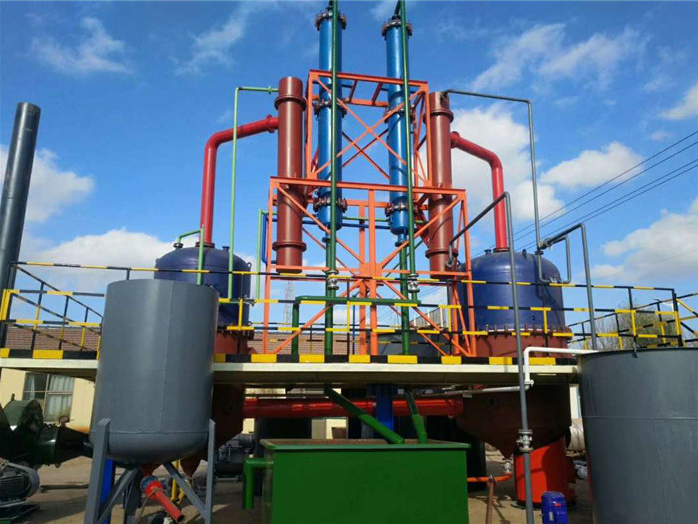
Magnesium chloride equipment features high efficiency, energy savings, stable operation, and superior product quality designed for severe environmental conditions.
May 11, 2025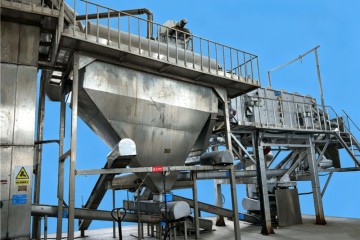
Multi-level vibrating screen and automatic packaging systems built for processing refined industrial salt.
Comprehensive equipment suite for washing, purifying, and processing food-grade and industrial-grade salts.

Anti-corrosion, wear-resistant, and food-grade conveying belts designed specifically for wet salt environments.
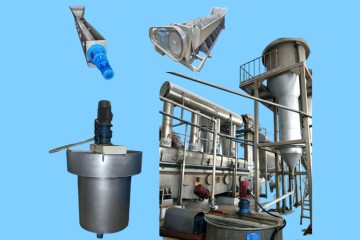
High-capacity salt purification machines and refined salt production line components.
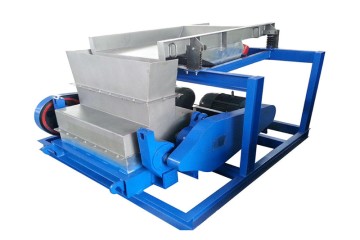
Heavy-duty crushing machinery optimized for breaking down raw mined salt blocks prior to processing.
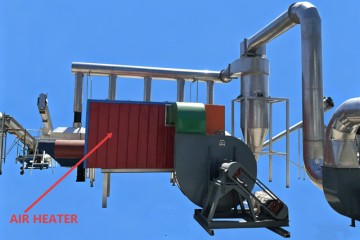
Fluidized bed and rotary drying systems engineered for high-efficiency moisture removal in salt plants.
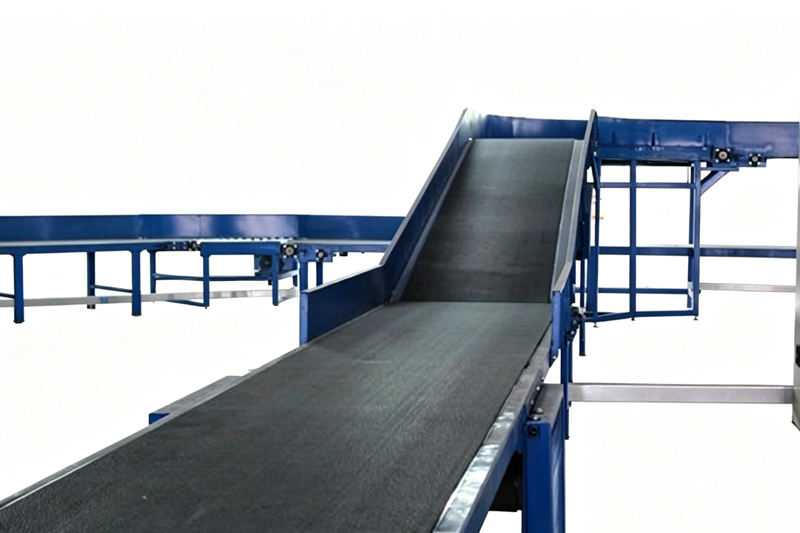
Widely used in mining, metallurgy, and chemical fields, designed for continuous conveying of lump and granular materials.
VIEW PRODUCT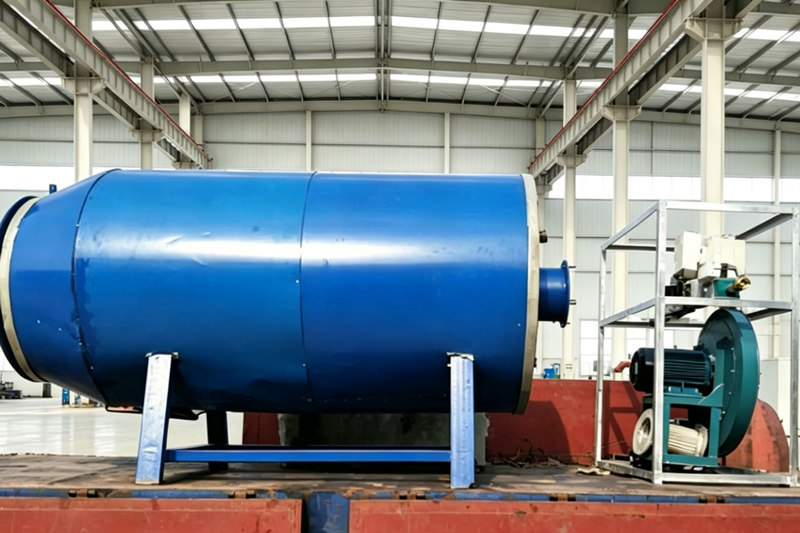
High-efficiency, energy-saving hot air furnace featuring precise temperature controls, adaptable to various fuel sources.
VIEW PRODUCT