


Leave Your Message
Engineered by Shandong Ruitu Automation, delivering verified thermal efficiency, continuous automated operation, and corrosion-resistant construction for demanding mining and chemical operations across Australia.
 Brand: Ruitu Automation | Origin: China
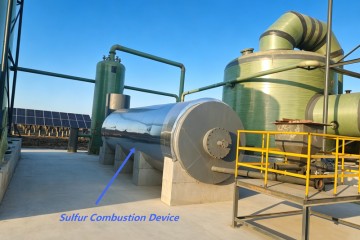
Continuous sulfur atomization and high-temperature furnace generating clean SO₂ gas streams with digital pressure control.
VIEW MORE Brand: Ruitu Automation | Origin: China
Complete industrial turnkey line engineered for salt lakes and seawater bittern, maximizing recovery rates under automated controls.
VIEW MORE Brand: Ruitu Automation | Origin: China
Core advantages include flexible raw material handling, tight energy consumption control, and high output purity matching industrial standards.
VIEW MORE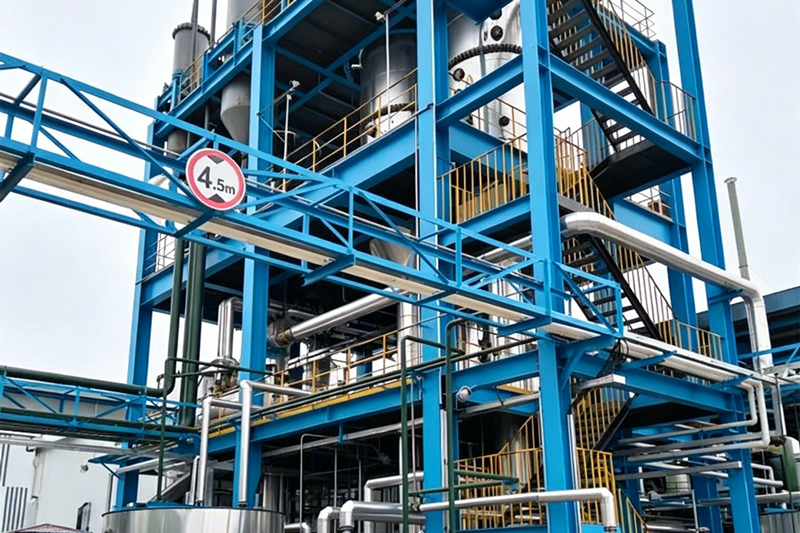 Brand: Ruitu Automation | Origin: China
Custom configured for seawater, sub-surface brine, hypersaline lakes, and magnesium-containing industrial by-products.
VIEW MORECombining rigorous Chinese manufacturing capacity with AS/NZS compliance protocols for extreme outback environments and coastal refineries.
Our sulfur combustion devices feature patented pneumatic/hydraulic dual-fluid spray atomizing nozzles, producing microscopic sulfur droplets that burn completely in refractory-lined furnaces above 1150°C, maintaining residual sulfur below 5 ppm and conversion efficiency above 99.8%.
Pressure vessels, combustion chambers, and skid pipes fabricated to AS 1210 and ASME VIII certifications. Electrical switchboards, motor control centers (MCC), and SIL-rated fail-safe interlocks comply with AS/NZS 3000 and Australian Hazardous Area classification directives.
Modules arrive pre-piped, pre-wired, and hot-tested at our 28,000 sqm Weifang manufacturing facility prior to shipment to Fremantle, Dampier, Brisbane, or Melbourne, drastically cutting on-site installation time and soaring Australian outback labor overheads.
The demand for high-performance sulfur combustion devices (commonly designated as sulfur burners or sulfur burning furnaces) in Australia is propelled by rapid developments in critical minerals processing, hydrometallurgy, water clarification, and agricultural soil remediation. As Australia consolidates its role as an international hub for battery raw materials—including nickel, cobalt, scandium, vanadium, and lithium—industrial processing facilities require reliable on-site generation of sulfur dioxide (SO₂) gas and subsequent sulfuric acid or bisulfite solutions.
Traditionally, remote processing complexes across Western Australia's Goldfields and Pilbara regions, South Australia's copper belts, and Queensland's mining corridors incurred prohibitive logistics expenditures hauling merchant liquid SO₂ in pressurized isotanks. The implementation of modern, modular sulfur combustion devices manufactured in China offers Australian engineers a reliable, cost-effective alternative: transporting solid elemental sulfur prills to site and combusting them on demand in automated furnaces to feed hydrometallurgical circuits.
High-pressure acid leach (HPAL) facilities and spodumene concentrate roasting facilities rely heavily on precise oxidation-reduction potentials (ORP). Our skid-mounted sulfur combustion furnaces deliver sulfur dioxide streams with variable volume controls from 5% to 18.5% SO₂ concentration, safeguarding sensitive hydrometallurgical stripping and precipitation balances.
In lateral nickel projects throughout Western Australia (such as Murrin Murrin and Ravensthorpe corridors), sulfur dioxide acts as a fundamental reducing agent to convert manganese dioxide contaminants into soluble states and prevent premature co-precipitation of valuable cobalt and nickel. The sulfur combustion unit operates continuously under strict stoichiometric controls to generate high-purity sulfur dioxide, directly absorbed into leach liquors or scrubbed into sodium metabisulfite slurries.
The conversion of alpha-spodumene to beta-spodumene requires acid roasting at temperatures hovering around 250°C. Advanced sulfur combustion systems coupled with waste heat boilers supply both the targeted SO₂/SO₃ reactive gases and high-pressure steam, closing the energy loop and significantly lessening operational carbon footprints in remote off-grid mining microgrids.
Australia possesses expansive hypersaline groundwater tables and extensive coastal salt harvesting projects in Dampier, Port Hedland, and Shark Bay. In bromine recovery processes, sulfur dioxide functions as an indispensable reducing agent in the blowing-out and absorption stages:
Br₂ + SO₂ + 2H₂O → 2HBr + H₂SO₄
Our proprietary sulfur combustion furnace ensures instantaneous, complete combustion, avoiding elemental sulfur sublimation that would otherwise foul delicate packed columns or contaminate downstream hydrobromic acid purifications.
Australian arable soil profiles in the wheatbelts of WA and southern NSW regularly suffer from alkaline imbalances and critical sulfur deficits. Localized fertilizer producers employ sulfur combustion units to fabricate sulfur-bentonite pastilles, ammonium thiosulfate (ATS), and sulfurous water irrigators to neutralize calcified water resources and upgrade plant phosphorus bioavailability.
The engineering landscape for sulfur burners serving the Australian territory is undergoing seismic technological shifts:
Sourcing sulfur burning systems from China requires deep engineering mastery of Australian statutory frameworks. Shandong Ruitu Automation implements strict compliance measures across design, fabrication, and documentation:
Founded in 2015, Shandong Ruitu Automation Equipment Co., Ltd. is located in Binhai Economic and Technological Development Zone, Weifang City, Shandong Province, covering an area of 28,000 square meters. With over a decade of hands-on expertise in salt chemical, thermal combustion, and hydrometallurgical equipment manufacturing, we are a reputable EPC contractor delivering total end-to-end industrial packages.
From feed chemical characterization, water analysis, plant site engineering, and proprietary equipment fabrication to Australian standard installation guidance, system commissioning, operator training, and lifetime parts replenishment, we provide dependable, turn-key solutions trusted across five continents.
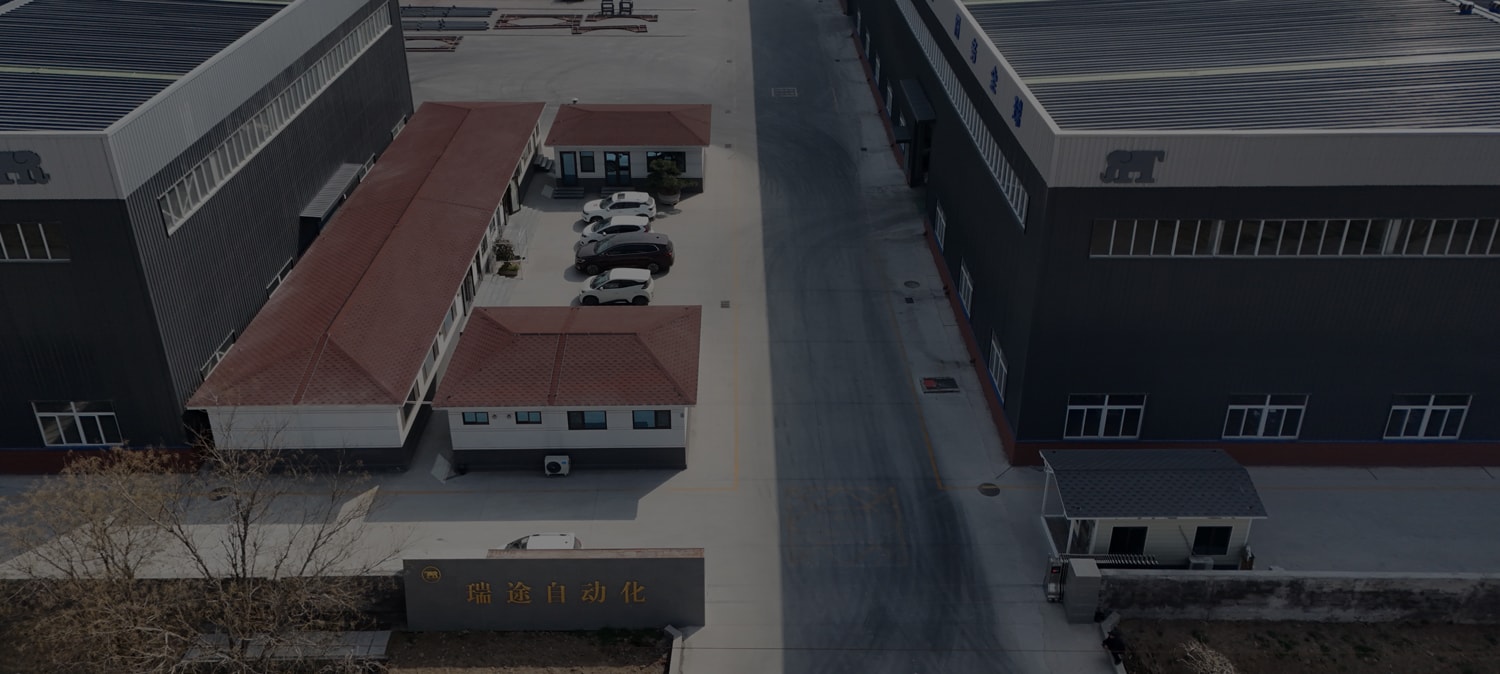
Structured execution minimizing client risk from early feasibility studies to on-site handover in Australian mining environments.
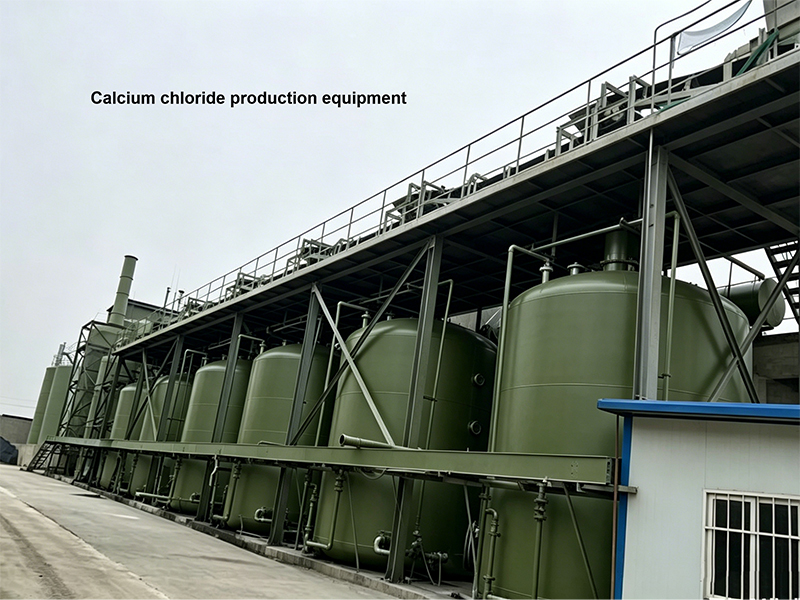
Technicians with extensive mineral and chemical experience analyze local brine, minerals, and site conditions, providing comprehensive feasibility analysis, process mass balances, and 3D plant engineering aligned with budget parameters.
VIEW DETAILS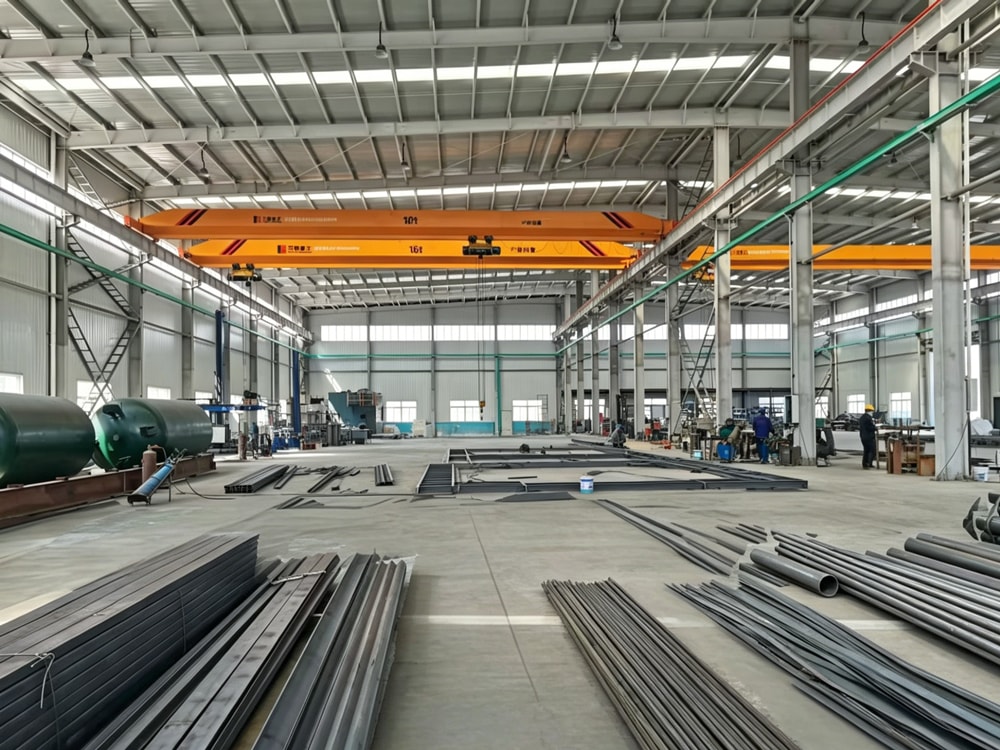
Utilizing our 28,000 sqm high-precision workshops and verified Tier-1 supply chains, we fabricate burners, reactors, scrubbers, and conveyors with strict QA/QC testing, material mill certificates, and ASME/AS dual compliance.
VIEW DETAILS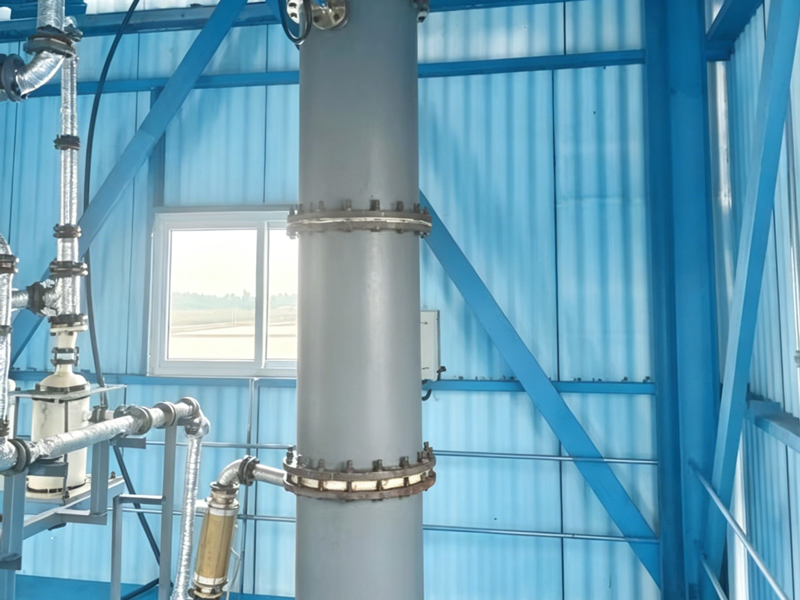
Complete mechanical and electrical site support. Expert engineers supervise assembly, cold runs, hot commissioning, and local personnel operations until targeted daily production yields and purity thresholds are attained.
VIEW DETAILSProven engineering implementations spanning chemical, mineral processing, and heavy processing complexes.
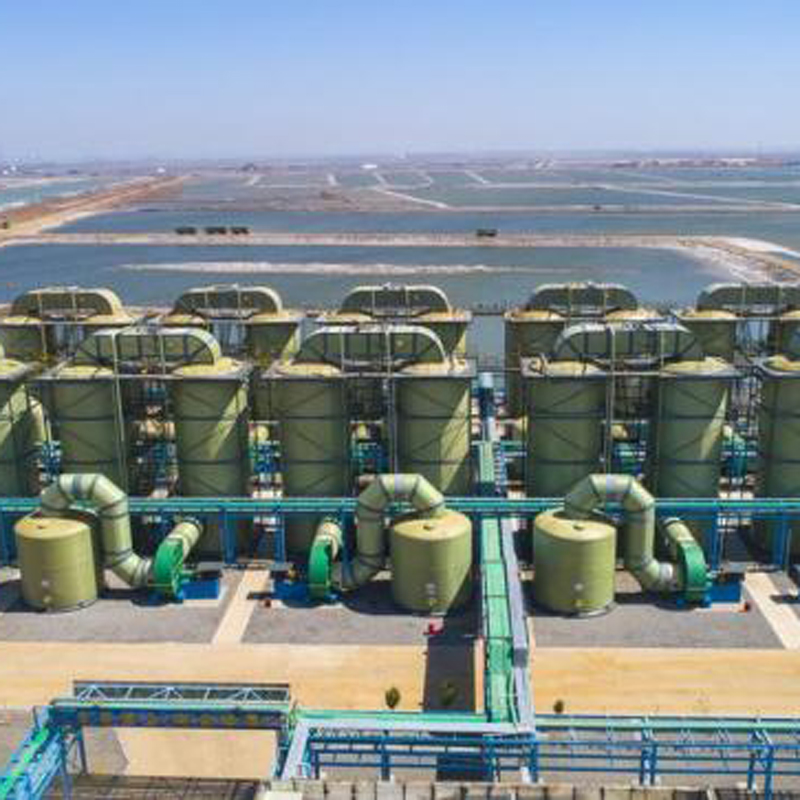
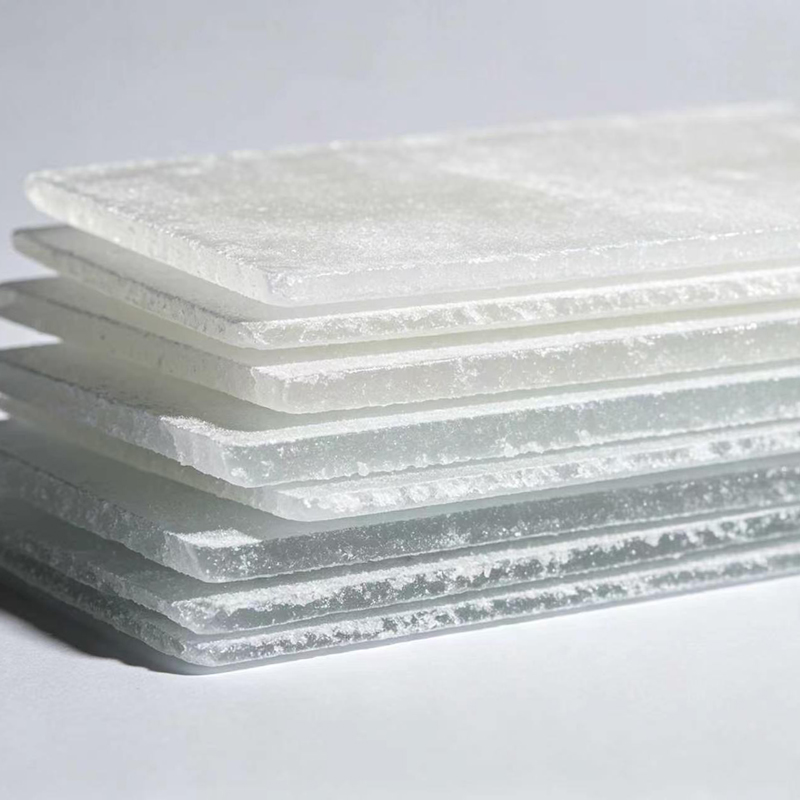
Turnkey plants delivered and operated reliably under severe climate and demanding chemical environments.
Bromine Extraction Project Case
Salt Washing Project Case
Salt Washing Project Case
Stay informed on process advancements, maintenance insights, and technological trends.
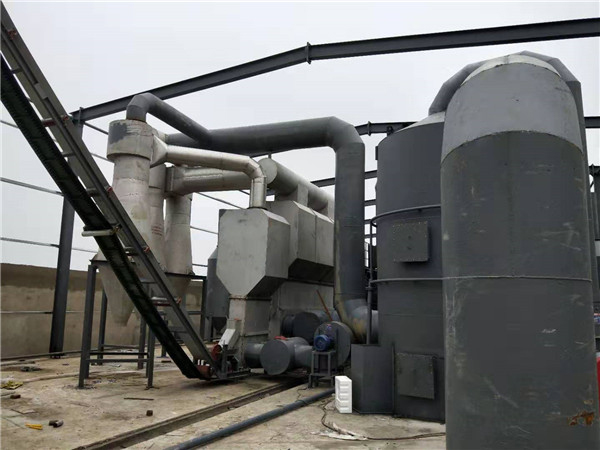
The chlorine gas calcium chloride process equipment consists of key components including reactor, absorption tower, and modular heat recovery units...
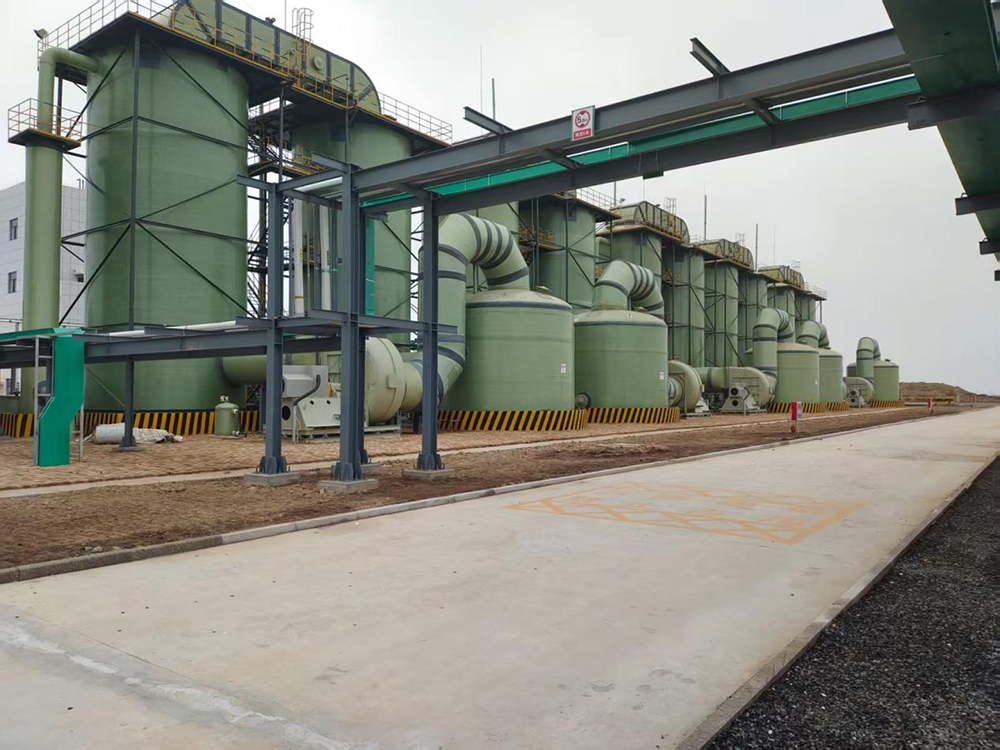
Bromine is known as the marine element, with over 99% of global reserves in oceanic water. Extraction processes depend on dependable sulfur burners...
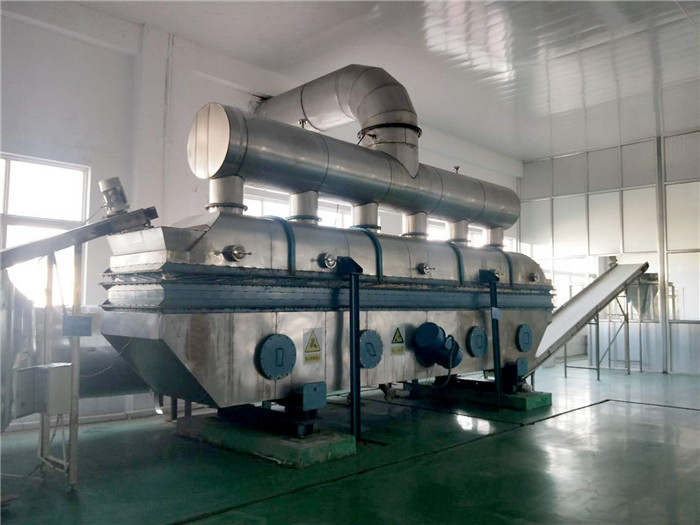
With continuous advances in fluidization thermal tech, specialized fluidized bed dryers optimize salt, chemical, and mineral crystal moisture removal...
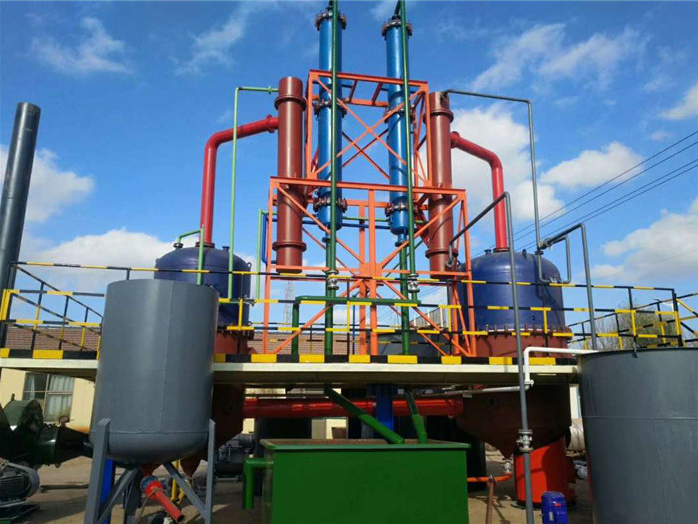
Magnesium chloride equipment features enhanced thermal efficiency, corrosion protection, continuous stability, and refined crystalline output...
Auxiliary machinery, crushing mills, industrial conveyors, and refining equipment designed for Australian harsh mineral environments.
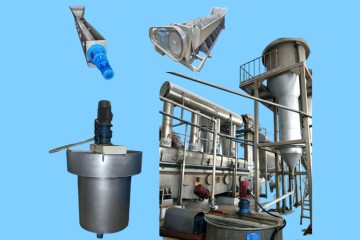
High-capacity salt purification machine for refined industrial and edible salt washing lines operating in coastal Australia.
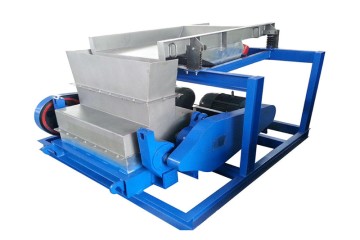
Heavy-duty double roll salt crushing mill engineered with anti-corrosion rollers to process raw mined and evaporated salt cake.
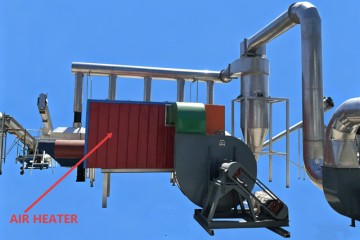
Continuous fluidized bed and rotary drying installation with high thermal efficiency for chemical grade crystal preparation.
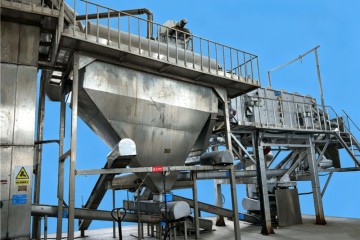
Multi-level vibrating classification screen paired with robotic bag filling for bulk chemical distribution.
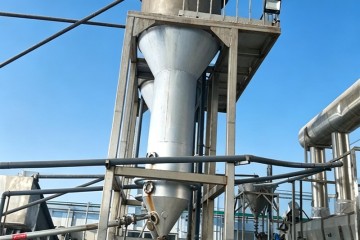
Integrated multi-stage counter-current wash system stripping magnesium and sulfate impurities from raw solar salt.

Corrosion-resistant, wear-resistant, and high-tensile material handling conveyor built for corrosive hypersaline environments.
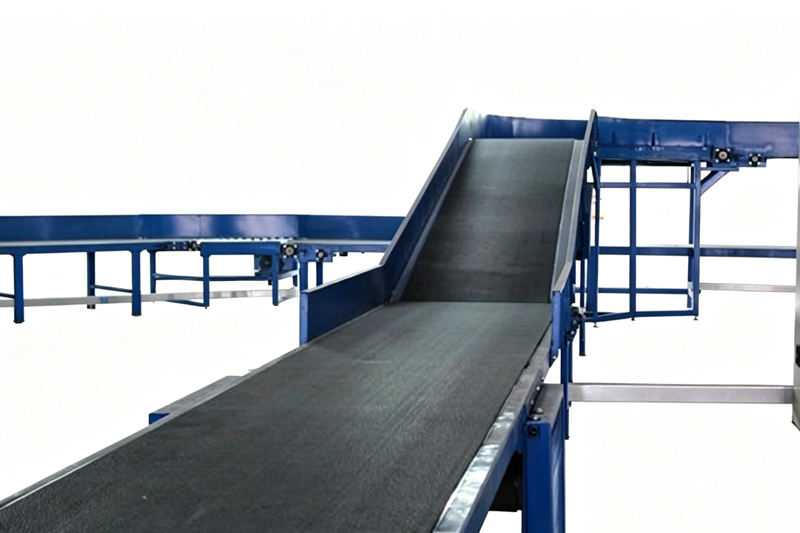
Engineered for mining, metallurgical, and chemical applications transporting lump, granular, and pulverized materials reliably.
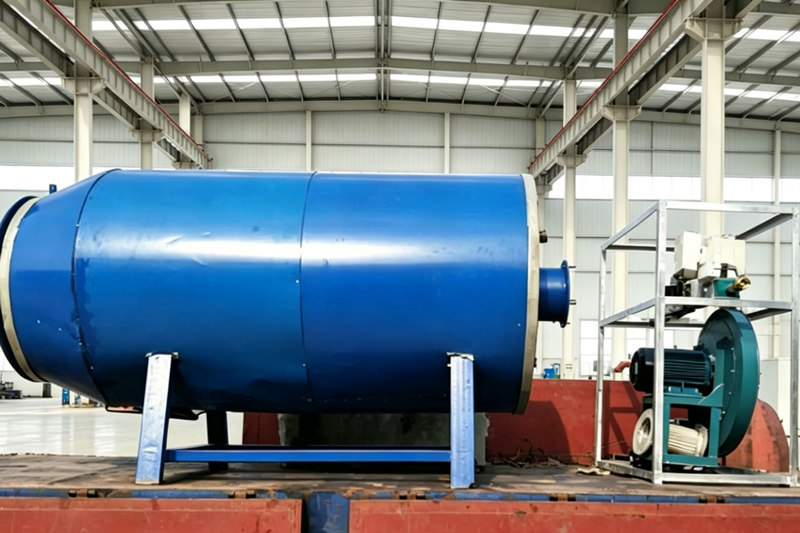
High thermal efficiency, tight temperature regulation, and versatile fuel adaptability for industrial mineral drying ovens.
Whether establishing an on-demand SO₂ generator for a nickel leaching facility in Western Australia, installing a sulfur combustion burner for a bromine extraction plant, or modernizing an agricultural nutrient pastillation setup, Shandong Ruitu Automation provides the engineering accuracy, manufacturing muscle, and export compliance your project demands.
Weifang City, Shandong Province, China | Direct Logistics Serving Fremantle, Brisbane, Sydney, Melbourne, Adelaide & Port Hedland