


China Custom Magnetic Conveyor Products, Factories
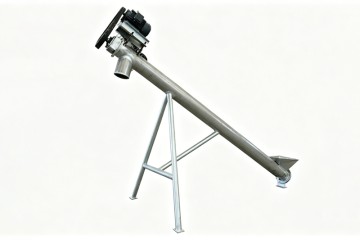
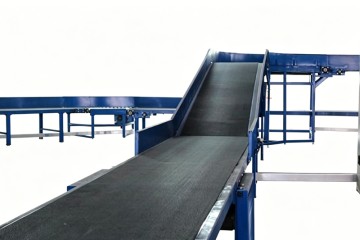
At Weifang Ruitu Automation Equipment Co., Ltd., we specialize in the design and manufacturing of high-quality custom magnetic conveyor products that cater to a wide range of industries globally. With a commitment to innovative solutions and superior craftsmanship, our extensive product lineup includes Helical Conveyors, Incline Conveyors, and specialized Conveyor Brushes, all engineered to streamline your operations. Our products are specifically tailored to enhance efficiency in material handling, ensuring that businesses can optimize their workflow and maintain a competitive edge in today’s fast-paced market, We pride ourselves on our state-of-the-art manufacturing facilities located in China, where we adhere to rigorous quality control standards. Our team of experienced professionals is dedicated to providing personalized service, working closely with clients to understand their unique needs and develop bespoke solutions. Whether you require a helical conveyor for intricate designs, an incline conveyor for space-saving logistics, or high-performance conveyor brushes for cleaning and maintenance purposes, Weifang Ruitu Automation Equipment Co., Ltd. stands ready to meet your demands. Partner with us to enhance your production capabilities and benefit from our commitment to excellence in automation technology

Popular Magnetic Conveyor Industry Leaders Delivers Unmatched Quality
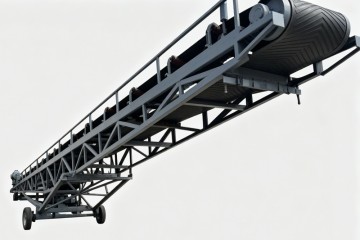
In the dynamic landscape of industrial material handling, the demand for high-quality conveyor systems has surged, particularly for specialized applications in sectors like bromine extraction. The growing popularity of various conveyor types, including the Pvc Belt Conveyor and Cleated Conveyor, has paved the way for innovative designs that enhance operational efficiency and product safety. Additionally, the integration of Conveyor Skirting serves to minimize material spillage and improve workflow, making these systems indispensable in modern production environments.
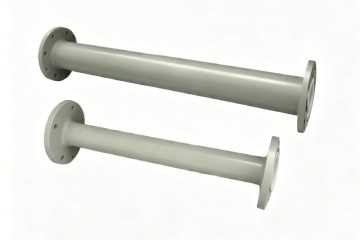
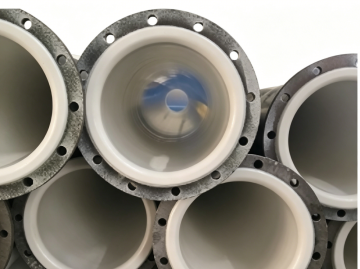
Furthermore, advanced materials such as the Ptfe Conveyor Belt and Lined Ptfe Elbow are enhancing the durability and chemical resistance of conveyors used in bromine chemical processing. Essential for ensuring precise handling of critical materials, Trough Conveyors, particularly in high-capacity settings, enable the seamless transportation of bromine crystals and other related substances. The ability to visualize complex systems through tools like the Bromine 3d Model facilitates better planning during the setup of these intricate processes.
Overall, the synergy between high-quality conveyor systems and cutting-edge bromine extraction technologies signifies a substantial advancement in the industry. With a focus on reliability and efficiency, companies can now leverage Aluminum Bromine and innovative solutions like the Incline Conveyor to streamline their operations and meet the evolving demands of global markets. The continuous evolution of these technologies will ensure that businesses are equipped with the tools needed for success in an increasingly competitive landscape.
Popular Magnetic Conveyor Industry Leaders Delivers Unmatched Quality
| Year | Market Size (USD Million) | Growth Rate (%) | Key Trends |
|---|---|---|---|
| 2021 | 250 | 5.0 | Automation Adoption |
| 2022 | 275 | 10.0 | Sustainability Efforts |
| 2023 | 300 | 9.1 | Digital Transformation |
| 2024 | 330 | 10.0 | Innovative Solutions |
| 2025 | 360 | 9.1 | Smart Manufacturing |

10 tips Magnetic Conveyor Pioneers in the Field in 2025
S
Susan Lee
Quality delivery on every level. The service team was very professional and handled my concerns swiftly and with expertise.
29
March
2026
T
Thomas Scott
Quality that really impressed me! The customer support team was very knowledgeable and answered all my questions promptly.
07
May
2026
B
Brian Rodriguez
Impressive quality and reliability. The after-sales support was prompt and well-informed, which made a big difference.
26
April
2026
K
Kevin Young
Outstanding quality. The knowledgeable after-sales team made my experience smooth and enjoyable.
06
May
2026
D
David Smith
Every detail of the product reflects high quality. When I reached out for assistance, the professionalism and expertise of the support team amped up my satisfaction.
15
May
2026
H
Henry Robinson
Truly a quality product! The expertise of their customer service staff made all the difference in enhancing my overall experience.
15
April
2026